

Automated Curved-Panel Line Qualification
During qualification trials on an automated production line for 100 mm curved sandwich panels, the Ecofoam® EC polyol system demonstrated excellent flow behavior and reliable cavity filling.
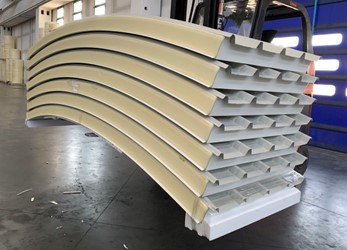
The trials identified demold time as the key process parameter influencing panel integrity. By extending demold time to approximately 35 minutes, the system eliminated core splitting and surface deformation, enabling consistent conforming panels at applied densities as low as 37 kg/m³.
With the process window now established, the next development phase focuses on optimizing green strength to reach the customer's standard demold cycle time while maintaining product quality.
Project Snapshot
| Application | Curved PU sandwich panels – 100 mm thickness |
| Production Environment | Automated molding cell with post-curing stations |
| Primary Objective | Validate a low-impact transition to Ecofoam® EC without disrupting production |
| Key Outcome | Stable panel production at 37–40 kg/m³ applied density. Cosmetic conformity achieved at approximately 35 minutes demold time. |
| Next Development Step | Reactivity tuning to reduce demold time while maintaining panel integrity |
The Production Challenge
Manufacturing curved PU sandwich panels presents several process-sensitive variables that directly influence panel quality. The customer needed to validate a new polyurethane system while maintaining stable production conditions on an existing automated line.
Key technical requirements included:
- Maintaining cosmetic surface quality on curved metal facings
- Ensuring uniform foam filling across complex mold geometry
- Preserving production cadence and automation stability
- Validating low-density capability without structural defects
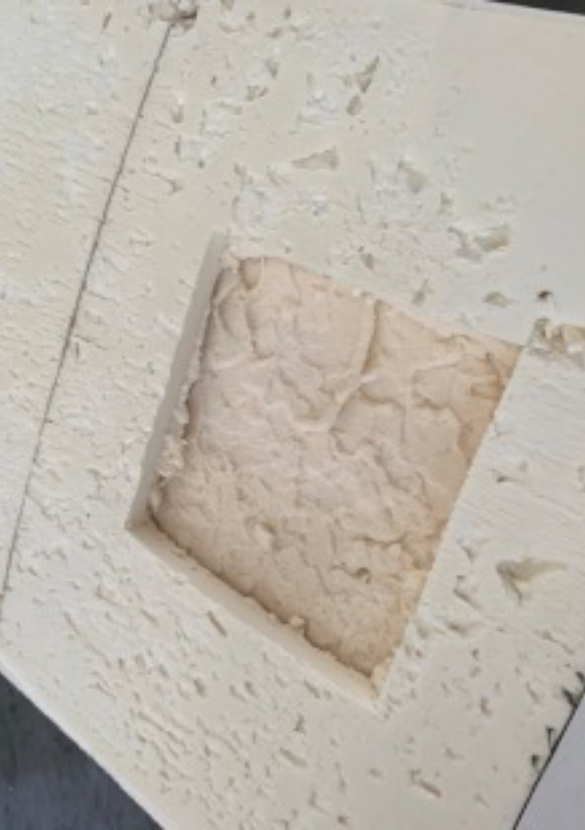
During early trials, panels demolded too early exhibited core splits and localized foam deformation, resulting in visible bulging on the metal skins. Identifying and stabilizing the critical process window therefore became essential.
The FSI Solution
FSI implemented a structured technical qualification and stabilization program designed to identify the controlling variables and establish a reliable operating window.
Technical Alignment
- Defined performance criteria and acceptance parameters
- Designed a structured trial and validation protocol
Controlled Production Trial
- On-site implementation on the customer's automated panel line
- Controlled system changeover with continuous process monitoring
Rapid Process Stabilization
Analysis of production data identified demold timing as the dominant variable influencing panel quality. By adjusting the demold cycle, FSI established a stable process window that eliminated internal defects and restored cosmetic panel conformity.
Evidence-Based Validation
- Production of 16 full panels for validation
- Reactivity testing and documentation
- Delivery of a technical evidence package for internal approval
Results
The Ecofoam® EC system demonstrated reliable processing performance and consistent panel quality under production conditions. Key outcomes included:
- Excellent flow behavior and mold filling across curved geometry
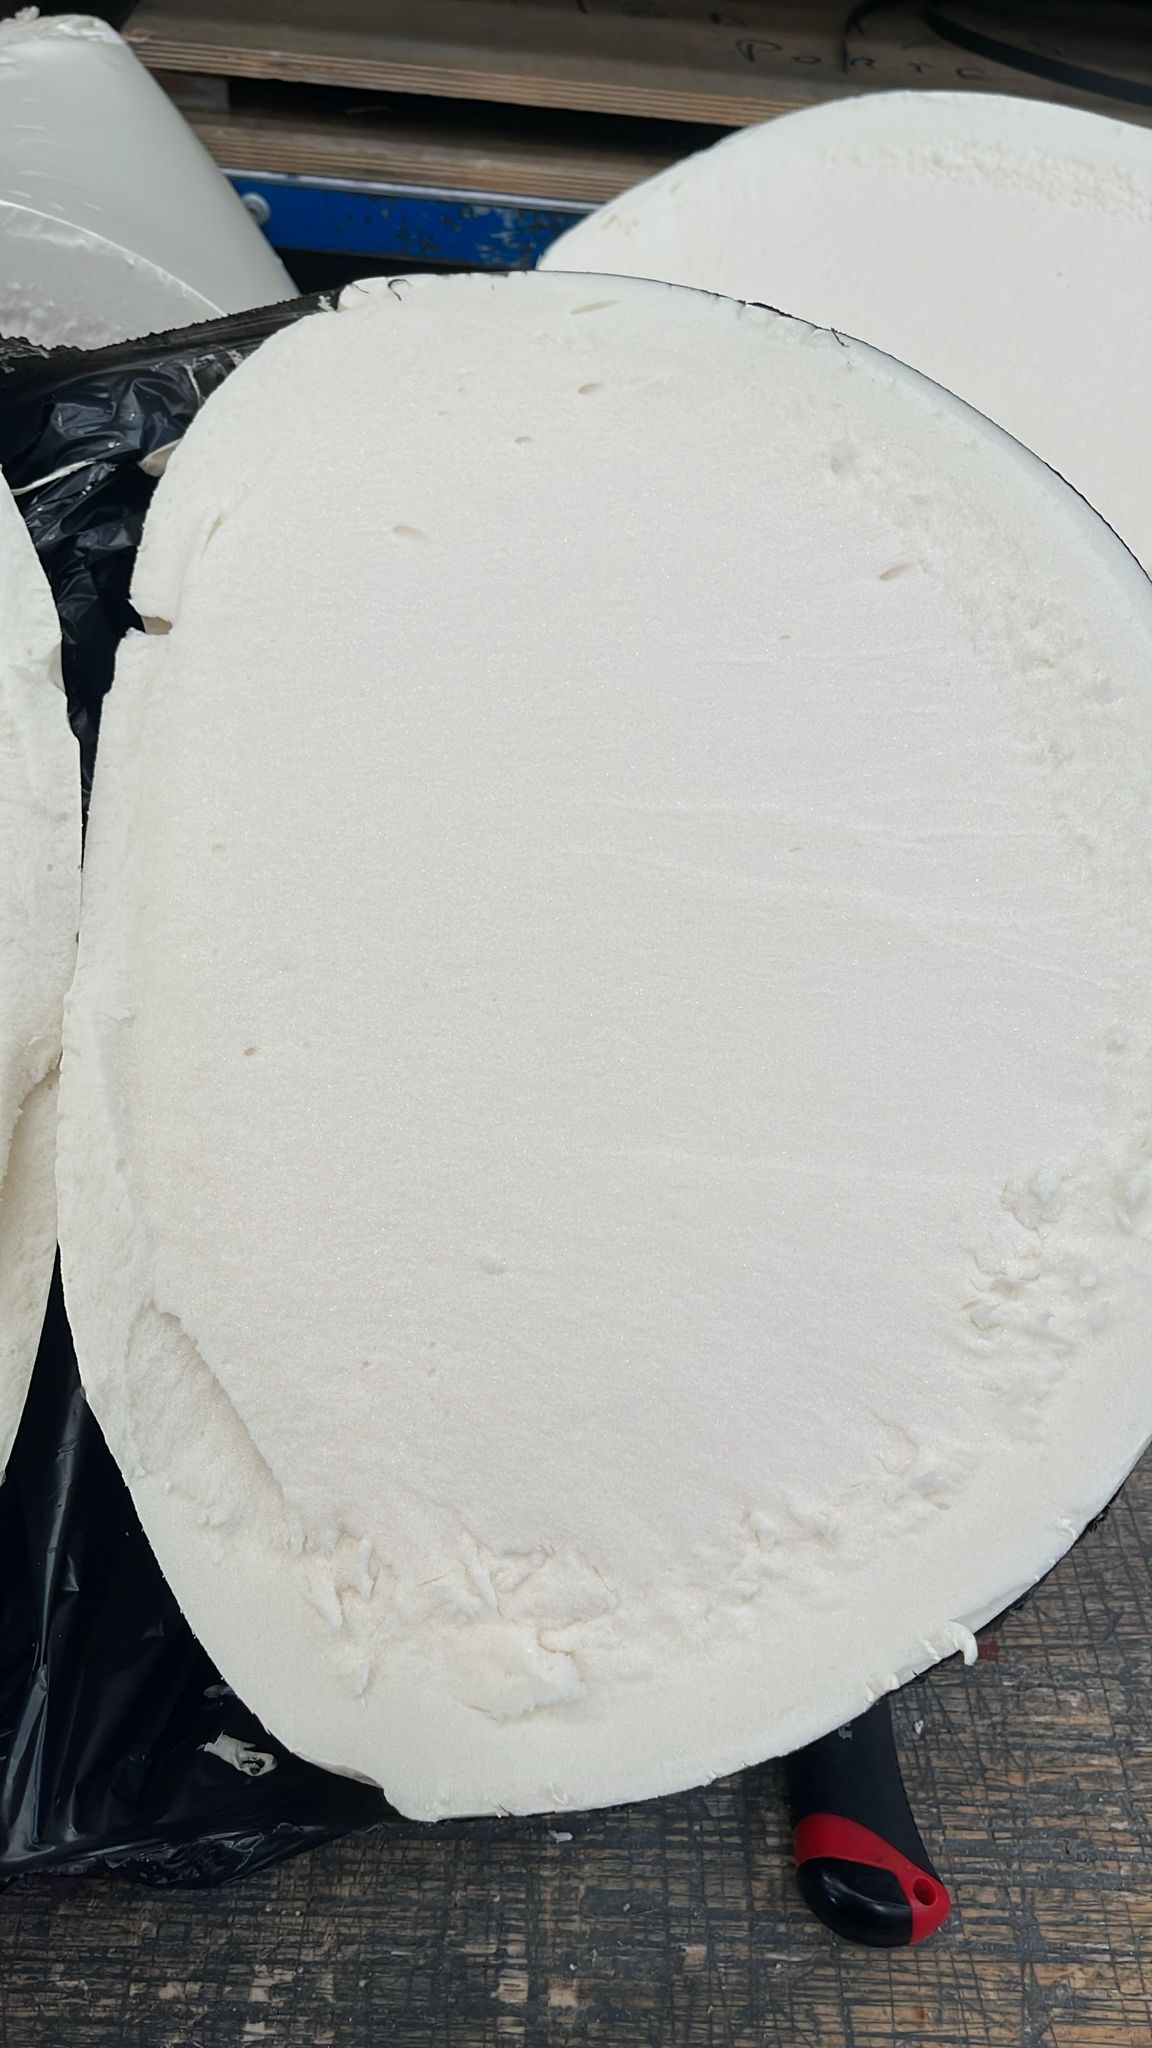
- Stable panel integrity with no core splitting
- Cosmetic conformity restored at optimized demold timing
- Applied density validated down to 37 kg/m³
The trials confirmed that process stability can be achieved without compromising density targets or equipment compatibility.
| Parameter | Result |
| Panel thickness | 100 mm |
| Applied density | 37–40 kg/m³ |
| Conforming demold time | Approximately 35 minutes |
| Trial production | 16 panels |
| Additional tests | Reactivity validation |
Visual Evidence
Customer Outcome
The trials confirmed that Ecofoam® EC can reliably produce conforming curved panels at the required density range on the customer's automated production line.
Through structured process analysis, FSI identified the critical process parameter controlling panel integrity and defined a clear stabilization window for production.
The next phase will focus on green strength optimization, enabling the system to reach the customer's standard demold cycle time without compromising quality.